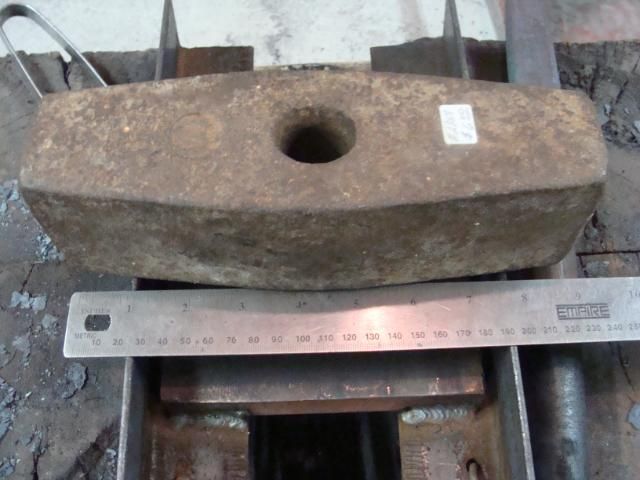
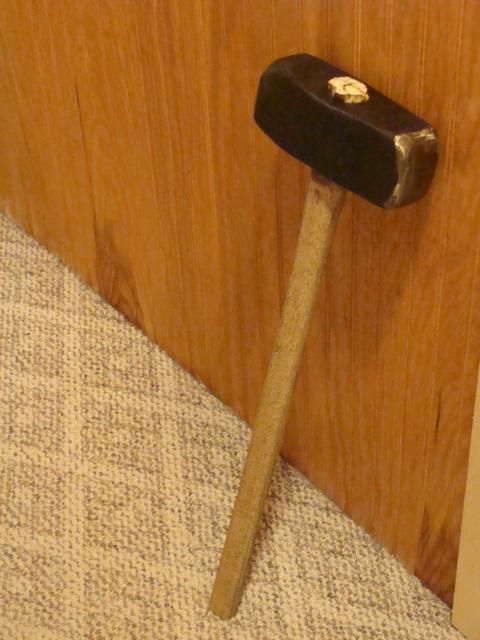
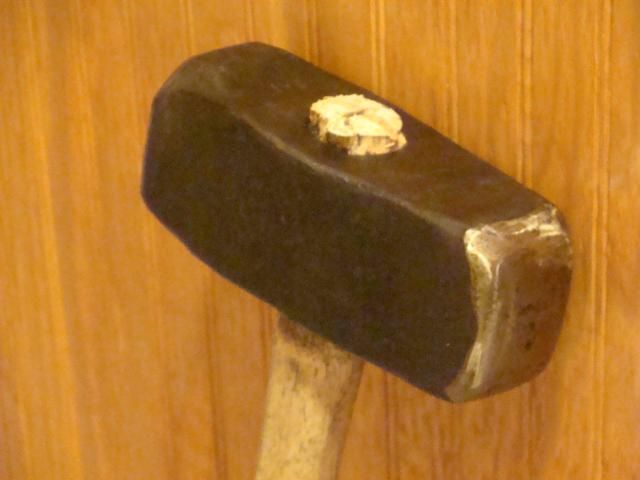
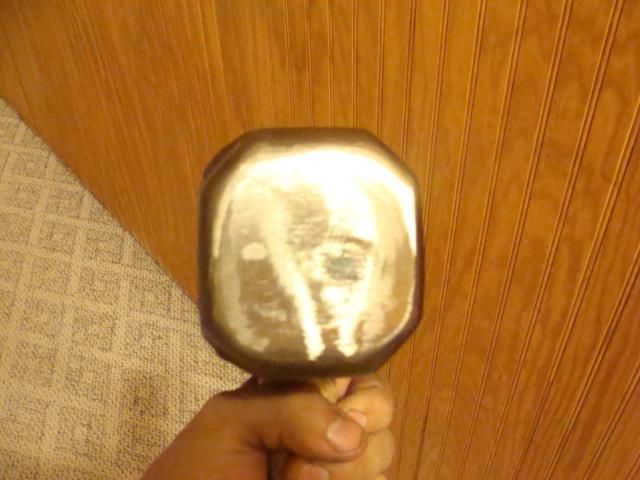
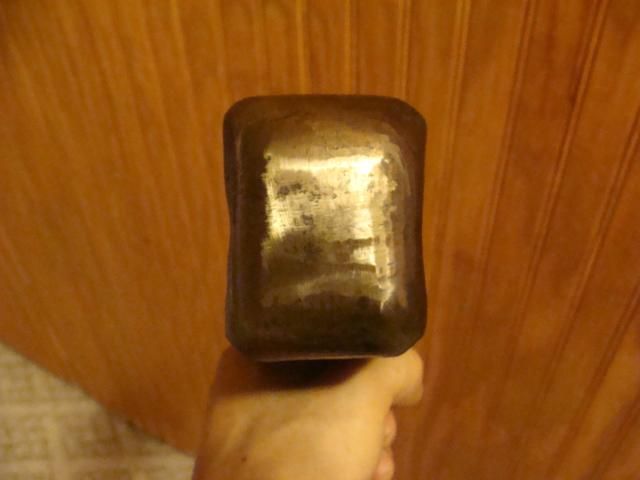
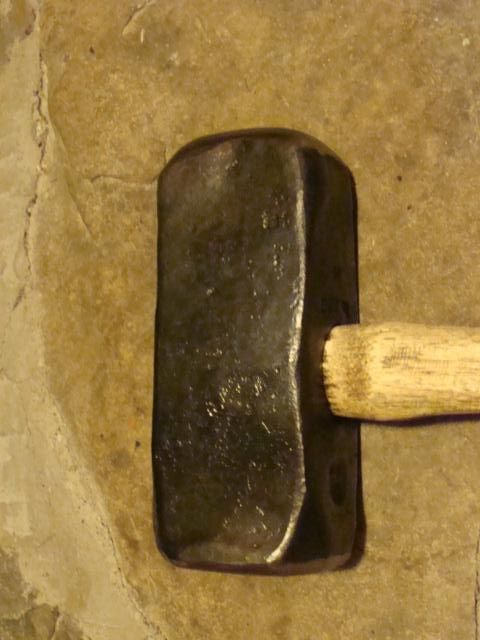
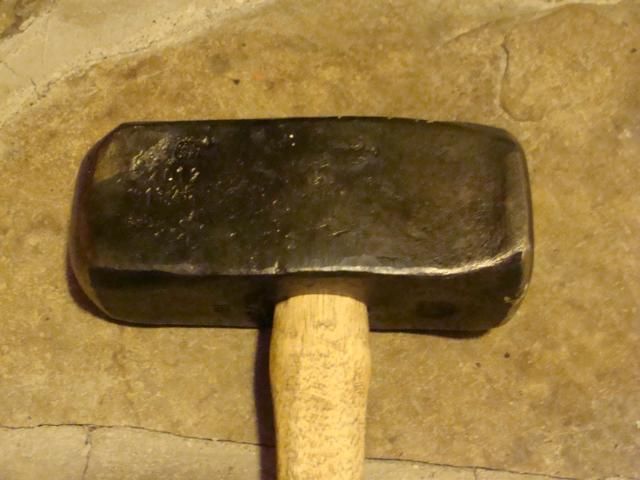
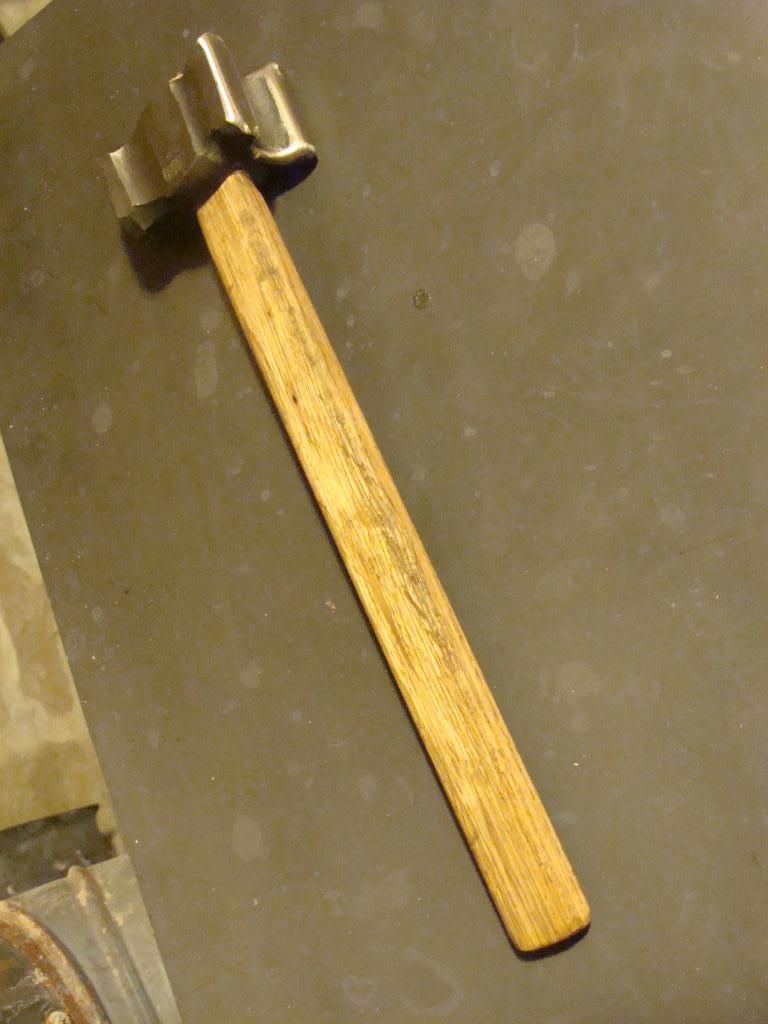
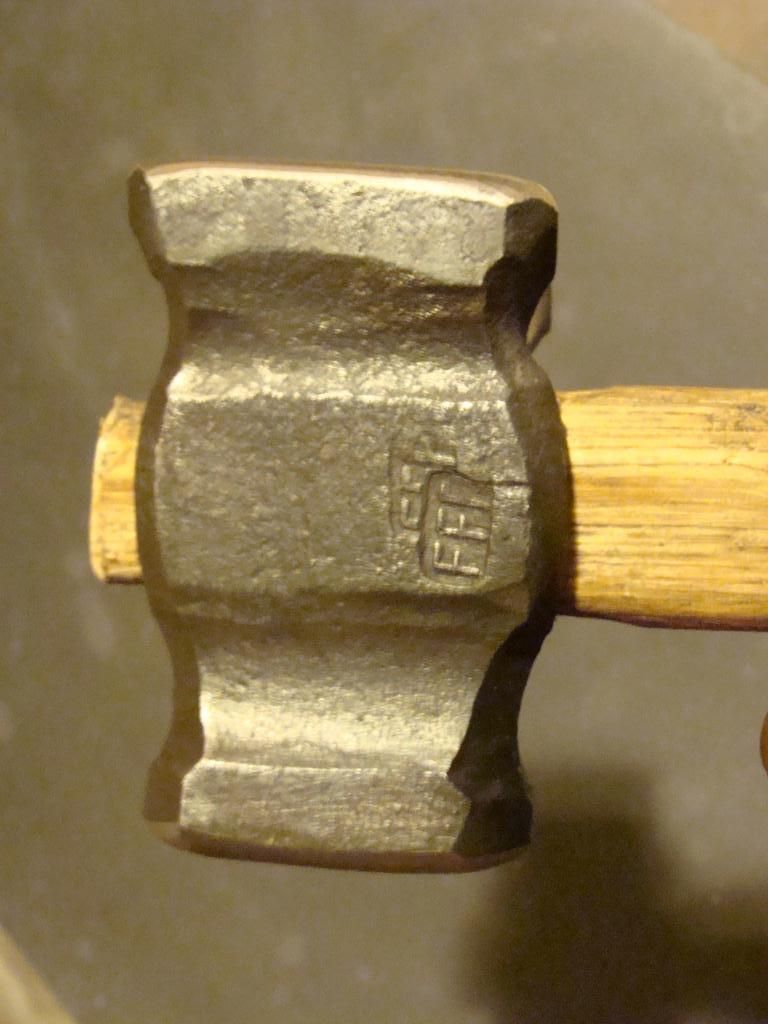
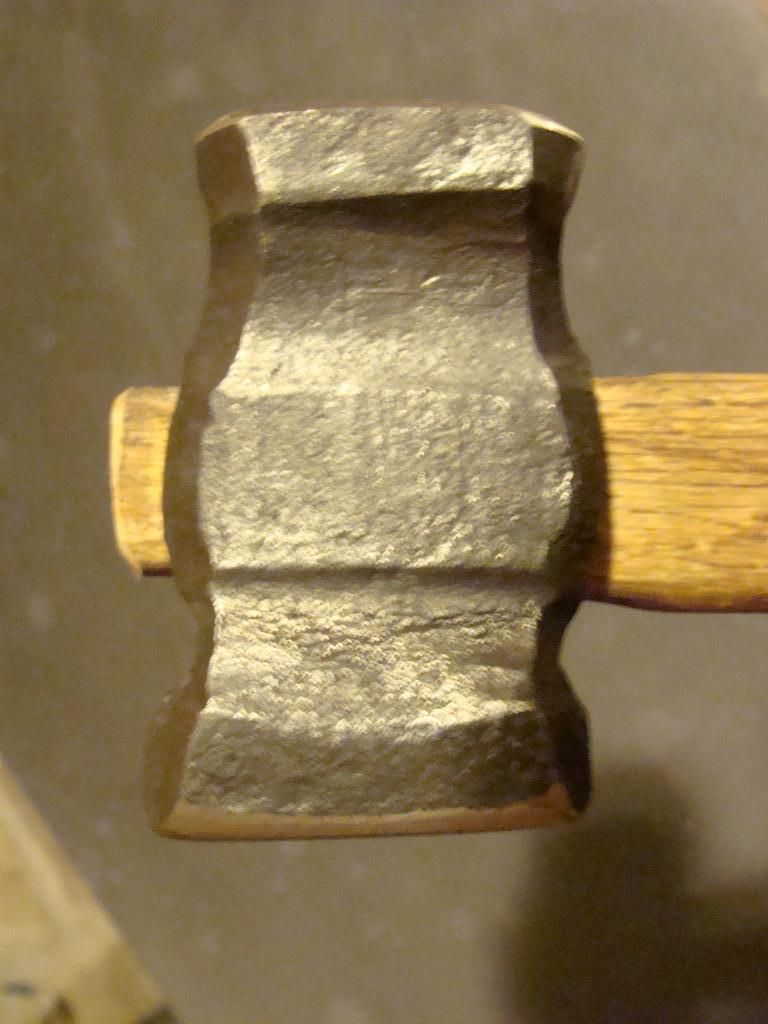
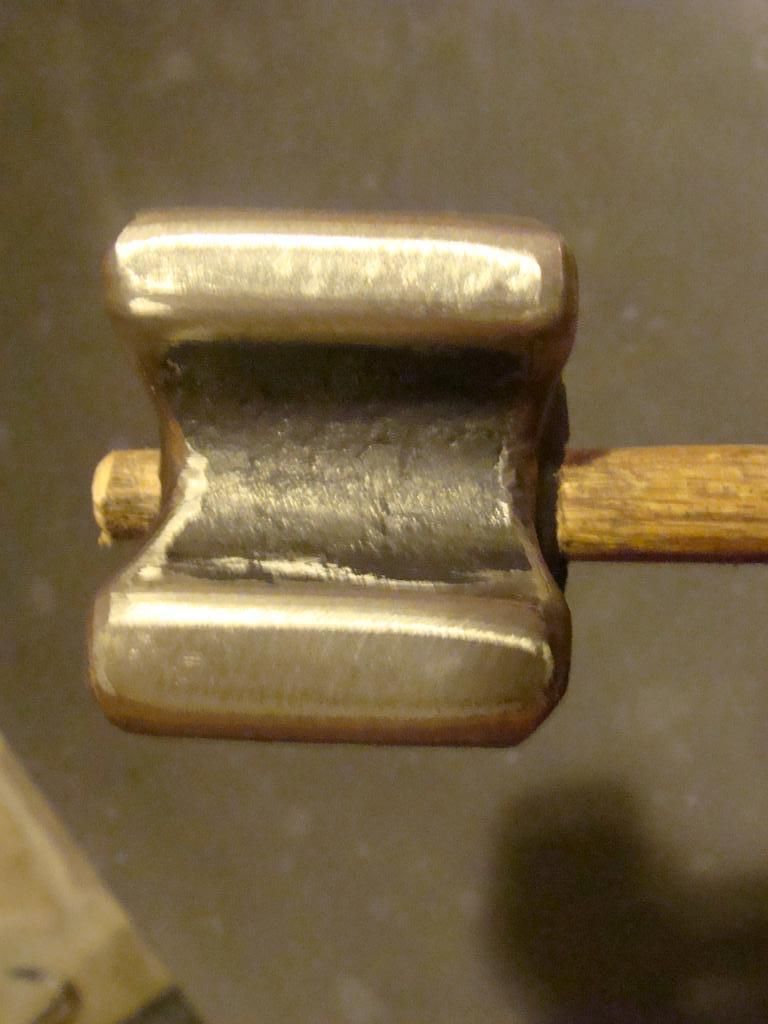
After the heavy forging Chase Saxton and I did, I realized I needed a second heavy sledge-hammer in my shop. I have a 10 pound sledge right now, that is a pretty decent one, but that's it. I stopped by the old antique store in town (where I got my last sledge head,) and picked up a 16-pound funny shaped sledge. It was all they had, but I figured with a little work, it would do.
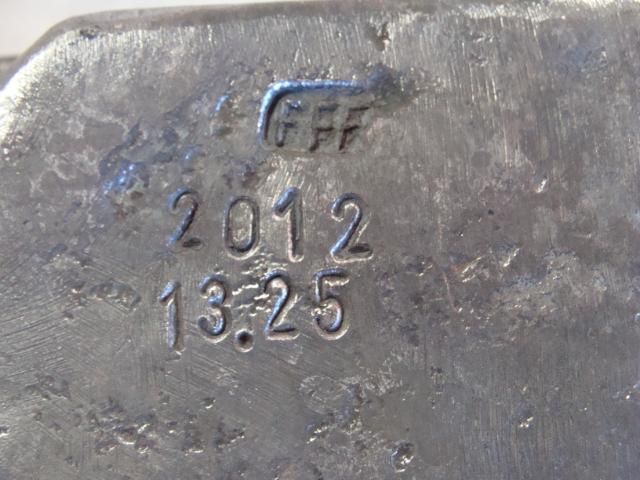
I sawed off the original faces to decrease the weight as well as to get rid of some chips and pitting. Then I set to work to shorten the hammer-head by "upsetting" the material. I made one of the hammer faces round and one face flat. By the time I cut, forged, and ground it into a usable piece of hardware, I had a 13.25-pound hammer head, that weighed 14.25-pounds with the handle.
Here is the original hammer head!
Here is a sped-up video of making the hammer-eye drift for this project, and then the work involved in upsetting such a large hammer head!
Here I am forging a "cupping tool" in the new striking anvil with the new sledge hammer.
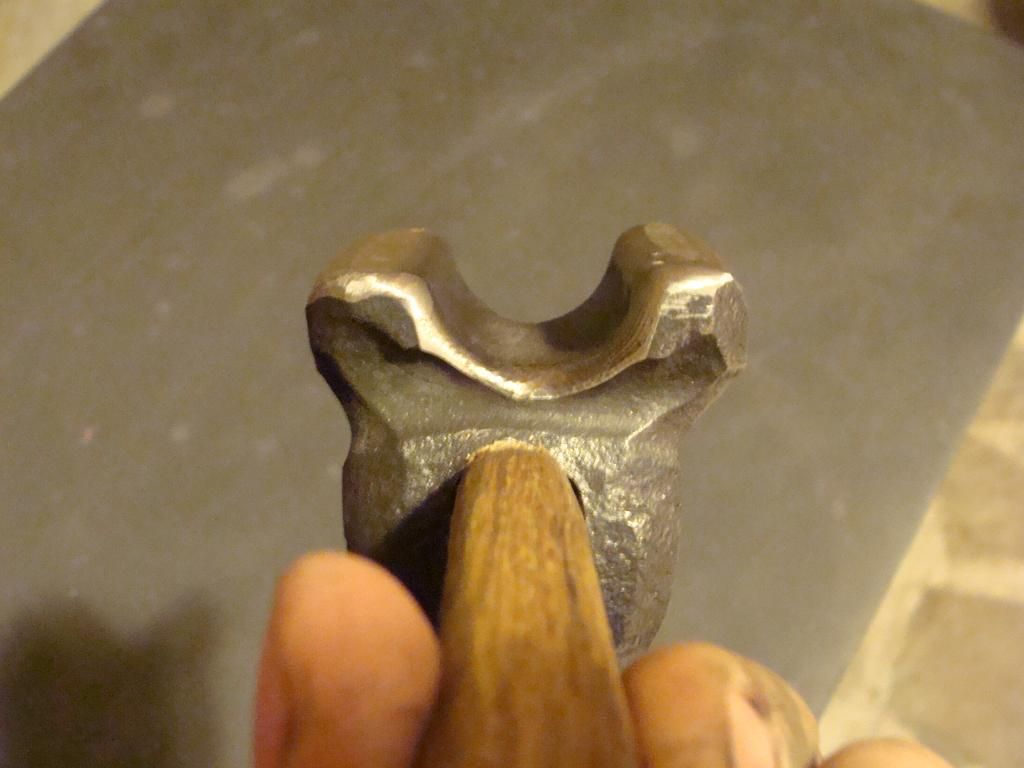
And yesterday I made my first "top-swage." Here are some pictures!
Well the title pretty much says it all!
Last week, I did some serious heavy forging here at the Fiery Furnace Forge Blacksmith LLC studio.
For some time now I have wanted a "striking anvil" for students to use when they come, and for myself when I make anvil tools. A "stiking anvil" is a flat, plain anvil made from cheap steel. The idea is, if a student swings a 12 pound sledge and misses the hot metal and slams it into the face or corner of your striking anvil, he may dent or break it, but it is an easy repair or a cheap replacement.
On the other hand, if a student misses and hits your real anvil and takes a chunk out of it, you've just broken a $500 shop tool.
So a striking anvil is a cheap and very smart investment. Plus in general tool making, it saves wear and tear on your anvil.
So last week, I up-'n-decided to make me a striking anvil.
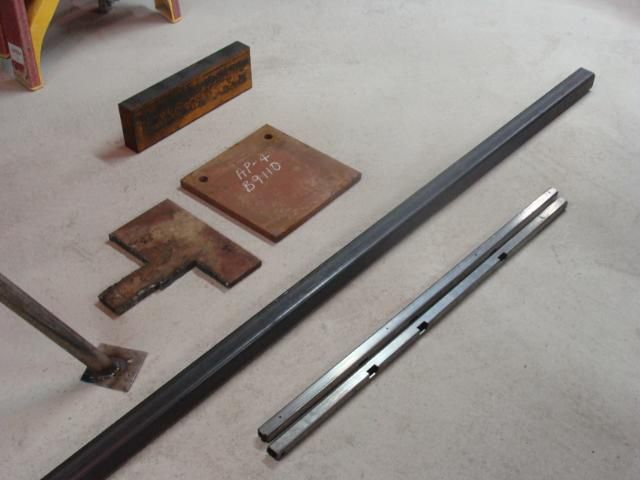
The venture began with a trip to the steel yard where I obtained the following materials.
2-inch square steel tubing for legs
3/4-inch thick plate steel for the anvil base
1-inch square tubing for leg supports
5/8-inch plate for feet
and a 2-inch x 5-inch x 16-inch solid piece of flat bar steel for the anvil itself.....this piece alone weighed 45 pounds.
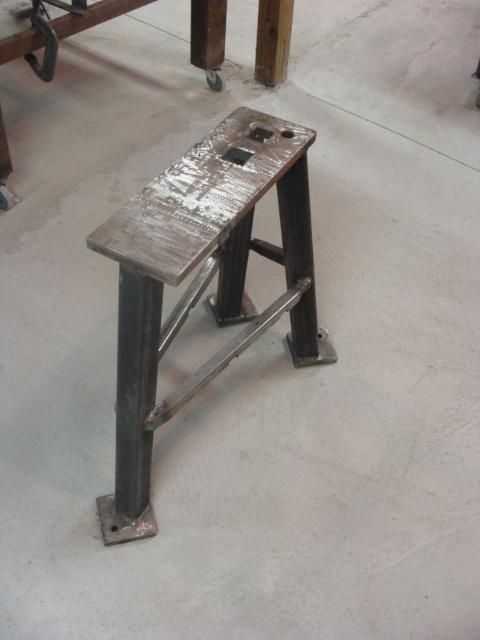
The next thing to do was build the stand for the anvil. This consisted of everything accept the flat bar piece that was the anvil iself.
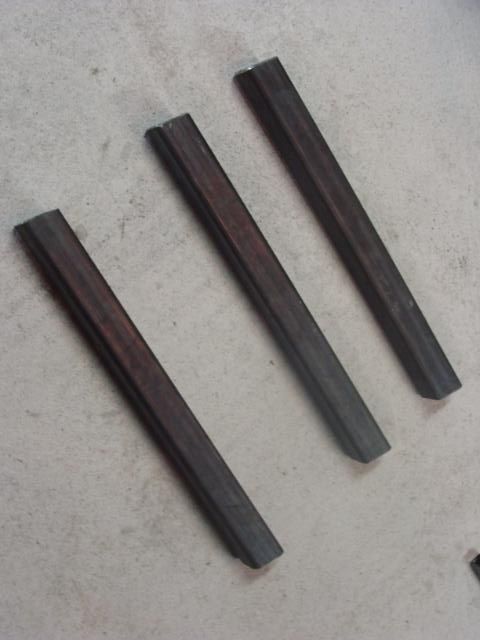
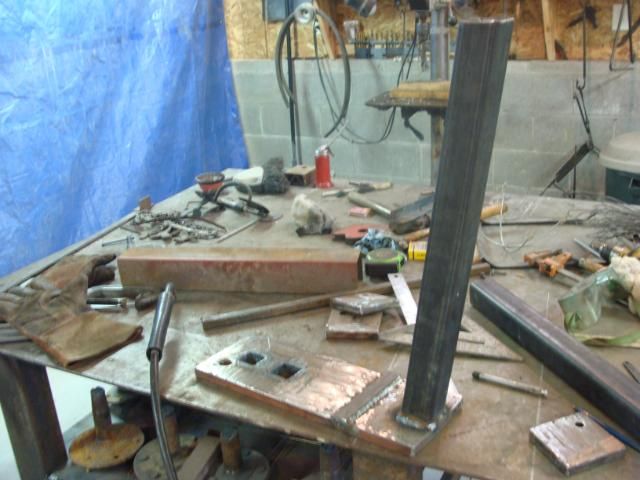
Legs!
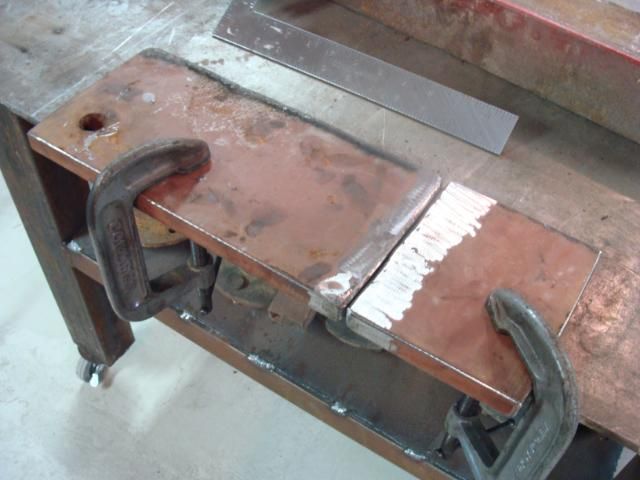
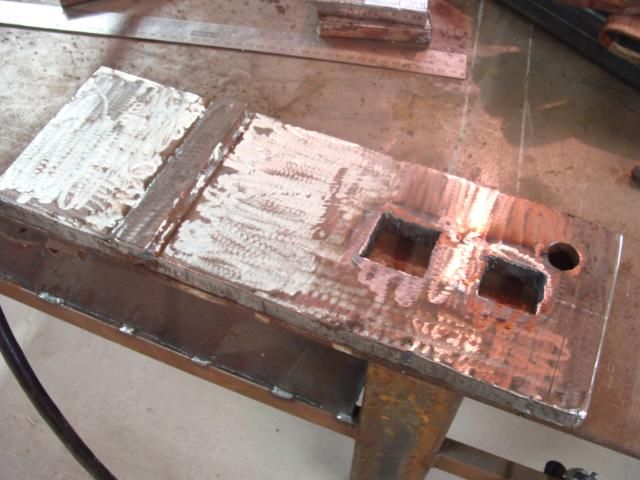
Base plate before welding and cutting!
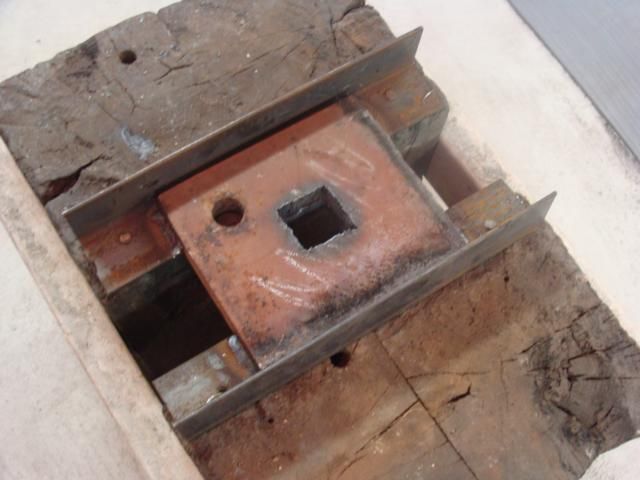
Base plate after welding and cutting. (Remember the square holes.....they are important.)
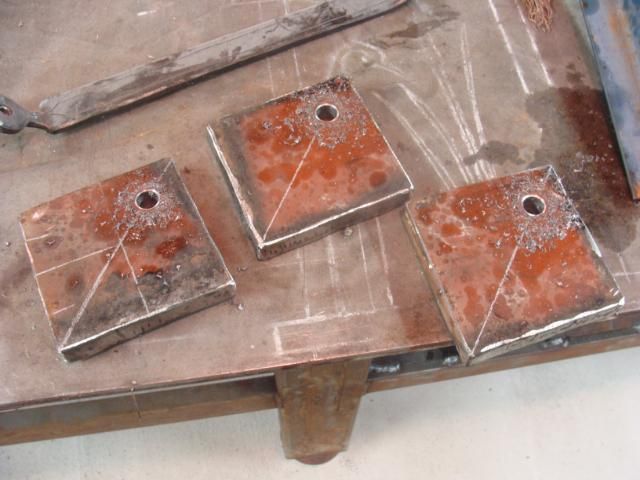
The feet! Notice the round holes....these are for bolting the stand down to the concrete, once it is finished!
One leg welded on! The legs are welded on at a 9 degree angle. This is an unimportant, unintersting fact that I just randomly decided to put in!
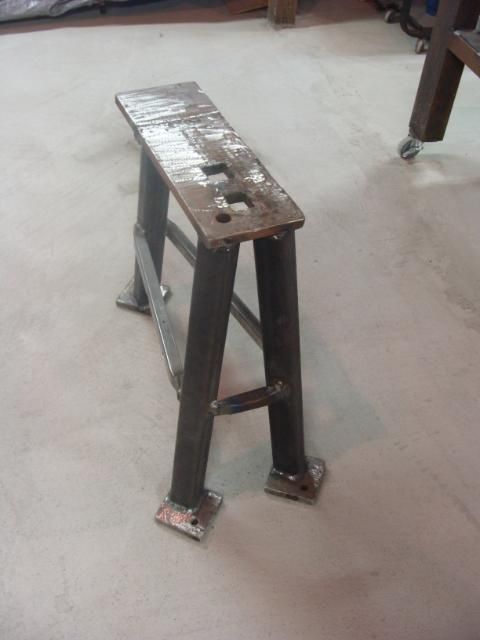
I kind of forgot to take some inbetween shots here. But basically the legs were filled with sand (to increase weight and decrease vibration,) then the feet and braces where welded on.
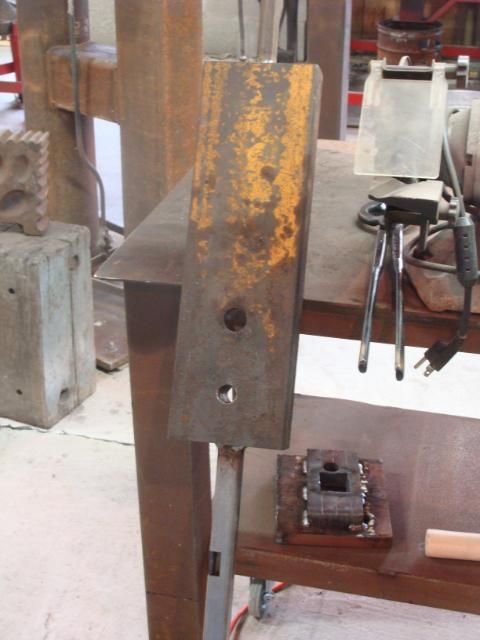
Now in an anvil, you have a square hole called a "hardy" hole. A large variety of tooling can be made for different processes, to fit in the hardy hole. So in order to make a striking anvil, I had to put at least one "hardy" hole in it. I decided to put two in mine. The standard hardy hole size is 1-inch so I decided to put a 1-inch hole in my striking anvil. My big shop anvil has a 1.25-inch hole though, so in order to make tooling for it, I decided to also put a 1.25-inch hole in my striking anvil. That is the reason for the two square holes in the stand. They are not the hardy holes, but they are clearance holes so that the base plate does not get in the way of the hardy holes in the actual "anvil." (Told you it'd be important!)
So anyway, there are two ways to get a square hole in a 2-inch x 5-inch x 16-inch chunk of steel. Hire someone to machine it.....perfect but EXPENSIVE, or "drill and drift" the holes yourself. I opted for the latter.
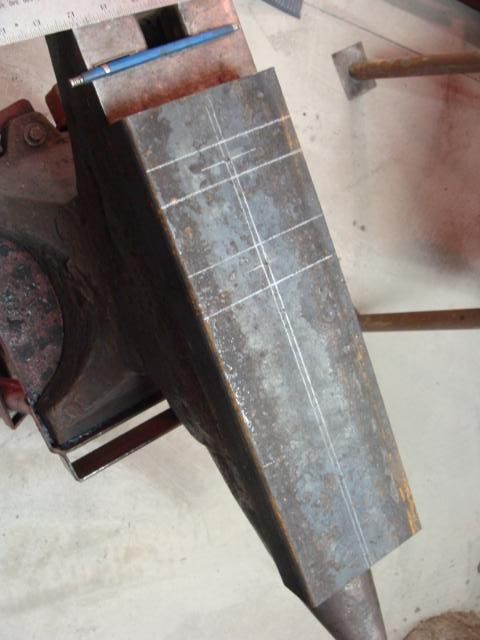
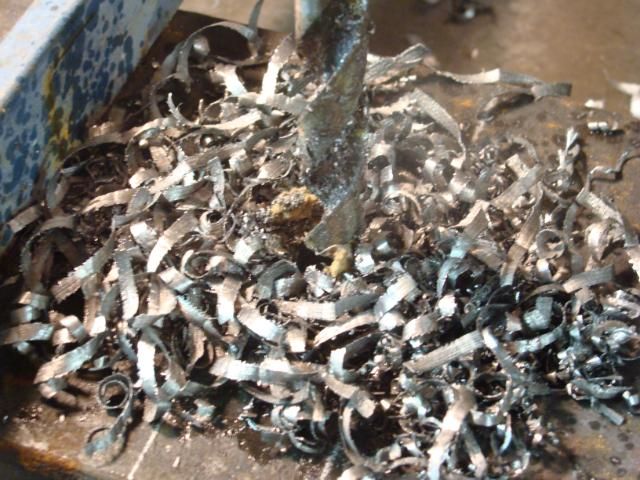
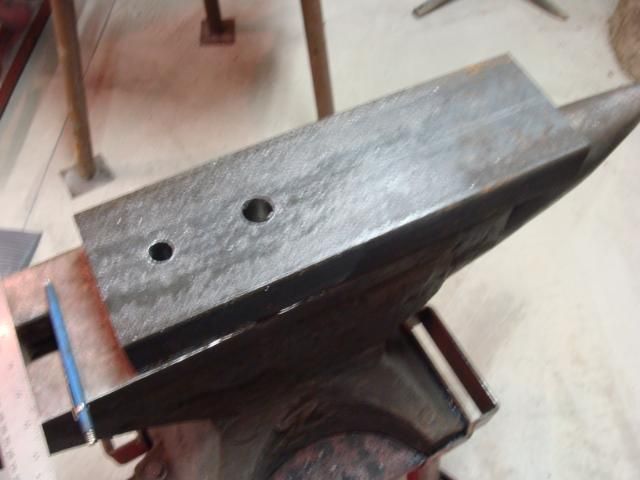
So what is "drill and drift?" Well drilling is the process of starting with a small drill bit and drilling a "pilot" hole through the material. Then you work your way up in consecutive sizes to the finished size. I drilled a 3/4-inch round hole where I wanted the 1-inch square hole to be, and a 1-inch round hole where I wanted the 1.25-inch square hole to be. It took about an hour to drill these two holes.
Marked for drilling!
During drilling!
Drilled!
Now what is "drifting?" Drifting is the process of taking a round hole, like the ones I drilled, heating up the area around the round hole, and then driving a square tool called a "drift" through the round hole. The square drift being the desired size of the finished square hole. In order to heat such a large and heavy chunk of steel up, I needed some handles on it. So I welded some scrap steel handles on.
Next I needed some way to support the piece while I drove the drift through. So I made this "make-shift" stand to get the job done.
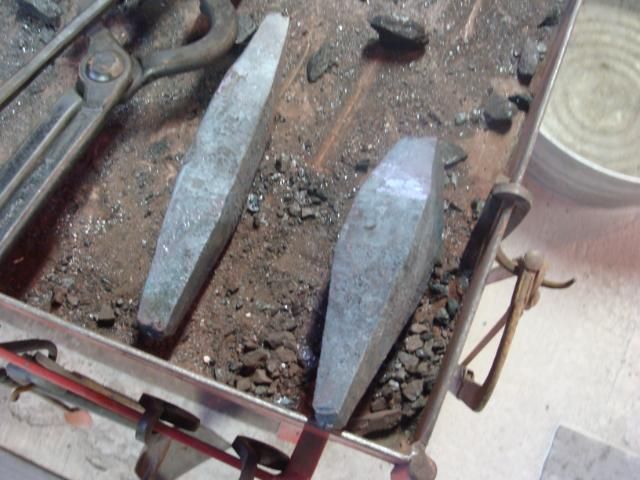
The drifts!
Now I knew I wouldn't be able to drive these gigantic drifts through this gigantic steel by myself. I needed a little extra umph, and extra hand, and an extra sledge hammer. I didn't need the extra ego, but that kind of came with the package! :D Enter Chase Saxton, my blacksmith friend from Bowling Green Ky.
I asked Chase to come over and help me drift the two holes square and then in exchange, we would make him a new forging hammer. He agreed, and came over to help with the big work. We did not take pictures of the process but we recorded it all and made some videos!
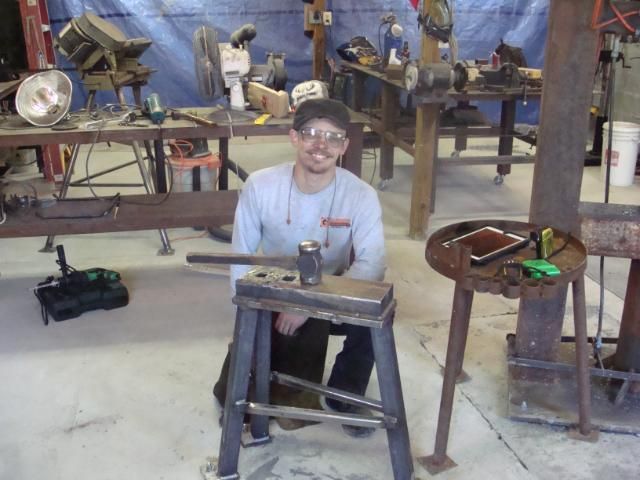
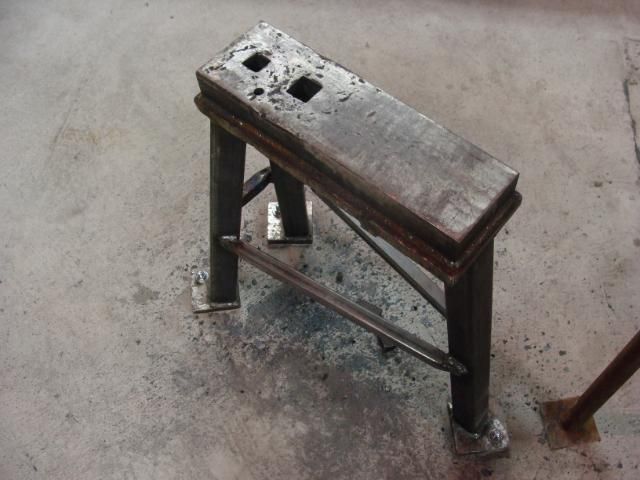
We got it all done and here are some pictures!
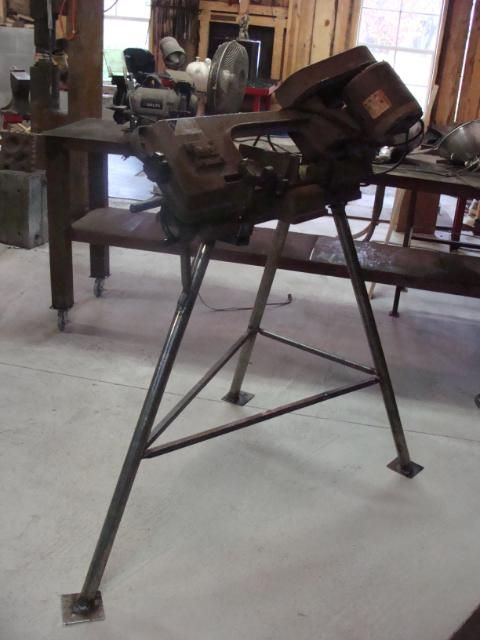
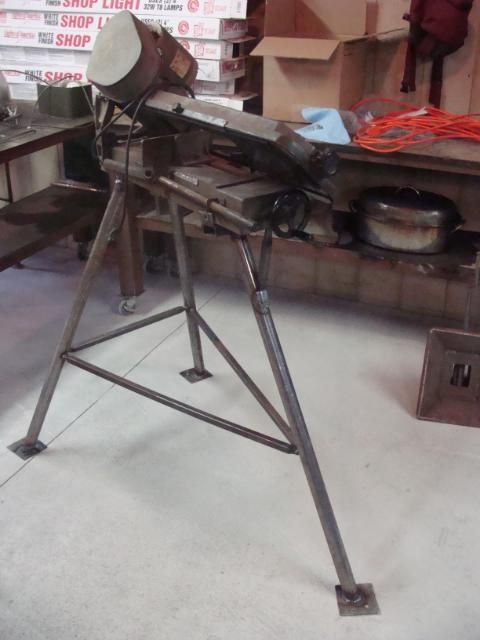
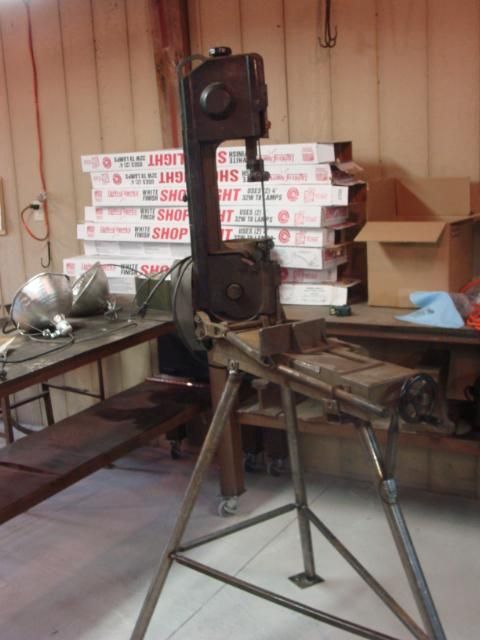
I also built a bandsaw stand last week! Here are a few pictures!
I do have some pictures of the hammer Chase and I made as well as some other heavy forging I've been doing, but this is all I have time for right now!
For those of you who do me the honour following my blog regularly, I must apologize! Things have been even more busy than before since my return from the young smith's trip through July and the early days of August.
Since then, my dear sister Kayla Custer got married off and now lives about 30 minutes away with her beloved hubby and my new Brother-in-law. She also has a baby on the way!
The beautiful bride!
The anctious groom!
Me escorting mom!
Uhhh "here comes the bride!"
My sister made her own cake!
The only thing I can say about this is that no-one will know what car I'm leaving my wedding in!
The weekend after the wedding, I had an art show in Louisville. As usual we set up our booth on Friday evening at the show. Friday night we were hit be a large and powerful storm, and despite having concrete blocks tied to every corner of both of my tents, they wre swept away and crushed by the wind. Other than this "small" misfortune, I did quite well at the show.
The week after the show we travelled to Colorado to visit Grandparents out there. We were there for about a week and a half. We had a good time site-seeing and such, and a highlight for me was being able to visit DRAGON FORGE, a large blacksmith shop in Pine Colorado! Here are a couple of pictures of me with the shop owner and his son!
When we returned from Colorado, I had another show to do with about three weeks to prepare. I had quite a bit of work to do, but was completely ready, and I also bought a new tent to replace the ones I had lost. We had a good show on Saturday, but Sunday was stormy and the show shut down early. That means every single show I have done this year has had bad weather on one of the two days.
After this show, dad and I spent a couple of days preparing the shop, and then we poured half of the concrete in the shop. This is something I have been planning for and saving for, for some time.
The week after this show I had another wedding to attend to. My good friend Miss Nicole, AKA the "goatgirl" of GOAT WAGON SUTLERS got married about a week and a half ago. I was asked by the groom to make a small goat sculpture for Miss Nicole. I spent a couple of days working on it, and I was very pleased with how it turned out. I believe both the bride and groom were very pleased with it too!
The groom requested that both the bride and groom's names and the date of marriage be stamped on the base plate of this piece. I emailed the bride and managed to get her signature for the names without her knowing what it was for. So the "Paul and Nicole" signature is the bride's hand.
After I returned from the wedding, dad and I once again, spent a couple of days preparing the shop (including moving my 1500 pound power hammer,) and then poured the second half of the concrete in the shop. The slab turned out very well, especially seeing that neither dad nor I have any experience pouring large quantities of concrete.
Currently, I am working to rearange the shop and get things back up and running. This involves moving equipment around, drilling holes in the concrete, and bolting down all of the heavy equipment. I currently have my forge, anvil, and power hammers back into position, but I still have to bolt them down. I have ordered a bunch of heavy-duty casters (industrial wheels for moving equipment on concrete surfaces,) and once they come in, I'll be putting them on my heavy tables.
Here are some pictures of the shop with concrete and a few of the tools back in place!
After I get my shop set back up and my primary tools back in place, I have some custom orders to get caught up on, as well as some other business ventures to puruse. Right now I've got work planned out a couple of months in advance, so I'm happy!
In the mean time, here are some more random pictures!